

Sprache
:

Sprache
:
3,4-Methyl hexahydrophthalic anhydride (MHHPA, CAS 25550-51-0) is a colorless liquid anhydride hardener of 50-80 cps at 25 °C. Assay is 98% minimum, the freezing point sits at or below -15 °C. Dosed at 110 phr in a 130 g/eq alicyclic epoxy, MHHPA yields about 123 mPa·s varnish for coil impregnation.
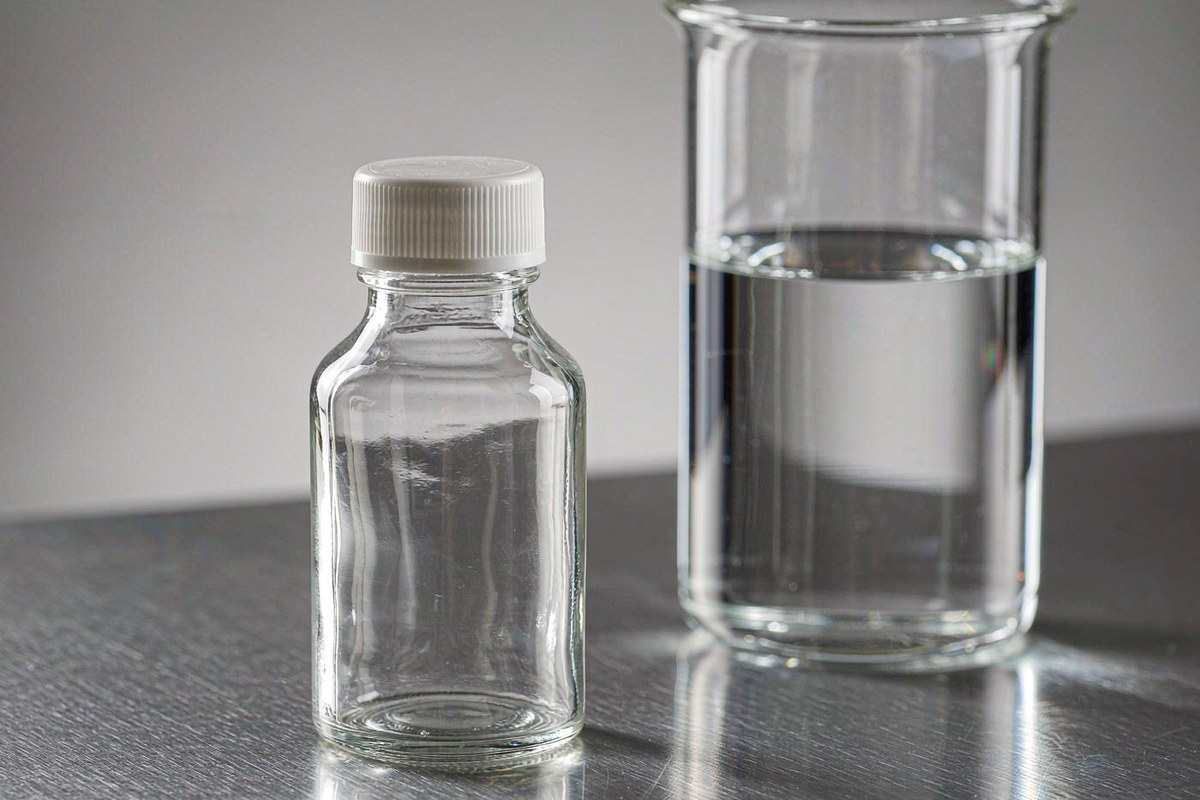
Figure 1. The published appearance of 3,4-methyl hexahydrophthalic anhydride is a colourless liquid, so the hardener is pumped and metered without a melting step.
Dry-type transformer coils, cast insulators and potted semiconductors ask the same thing of a resin: flow into a tight winding, then hold electrical strength at temperature. Anhydride-cured epoxy answers with a slow, low-exotherm cure and an ester network that stays stable when hot.
The liquid member of that family, MHHPA runs at 50-80 cps with a freezing point at or below -15 °C. An unheated drum stays pourable through most of a northern winter.
The cost sits in the oven. An anhydride does not gel at 25 °C in a useful time; it needs a warm tank and a staged cure. Data come from the MHHPA product page and the resin pages compared here.
Table 1 reproduces every specification line the page carries for 3,4-methyl hexahydrophthalic anhydride; nothing outside it is treated as a specification.
Table 1. Identity and published specification of 3,4-methyl hexahydrophthalic anhydride (MHHPA).
Item |
Published value |
Product name |
3,4-Methyl hexahydrophthalic anhydride (MHHPA) |
CAS No. |
25550-51-0 |
Appearance |
Colorless liquid |
Color, Pt-Co |
Max. 50 |
Content, % |
Min. 98 |
Viscosity, cps at 25 °C |
50-80 |
Freezing point, °C |
Max. -15 |
Iodine value, g I2/100 g |
Max. 1.0 |
Packaging and shelf life |
Drums and IBC tanks; 12 months in original packing |
Storage |
5-30 °C, dry, away from oxidants and acids |
Three data classes appear here, and a buyer should keep them apart.
Page values are the ten lines in Table 1. Calculated values are the anhydride equivalent weight of 168.19 g/eq, from C9H12O3 with one anhydride group, plus every mix viscosity in Table 3. Empirical values, such as the 0.85 factor and accelerator levels, are starting points.
Water is determined by Karl Fischer titration according to ASTM E203, and resin epoxy equivalents follow ASTM D1652 or ISO 3001. Flash point is not published; take it from the MSDS, determined according to ASTM D93 or ISO 3679.
Every calculated number can be reworked from the equations in section 4.
MHHPA cures epoxy through an anhydride ring rather than an amine hydrogen, and that difference accounts for the viscosity, pot life and heat resistance compared in Table 2.
Cure starts from a hydroxyl, not from the hardener. A residual hydroxyl on the epoxy, or a glycol added on purpose, opens the ring into a monoester carrying a free carboxyl.
That carboxyl opens an epoxy group into a diester and regenerates a hydroxyl, which opens the next anhydride. The sequence repeats into a polyester network.
Two follow. There is no fast amine-epoxy exotherm, so a thick casting does not run away in the mould. And no free amine is left to blush, so clear castings stay clear.
In practice an accelerator is still needed: tertiary amines or imidazoles at 0.5-2 phr cut gel time from hours to minutes at 120 °C. That band is an empirical starting point.
Overdosing it is the classic mistake. The mix gels in the pot, and the casting yellows.
Against the two amine hardeners used with the same YLCE-2021 alicyclic epoxy, MHHPA asks for more mass but returns a thinner mix.
Table 2. MHHPA against two modified cycloaliphatic amine hardeners on YLCE-2021, a 130 g/eq alicyclic epoxy.
Property |
MHHPA |
||
Hardener type |
Anhydride |
Modified amine |
Modified amine |
Appearance |
Colorless liquid |
Clear pale yellow |
Transparent viscous |
Colour limit |
Pt-Co max. 50 |
Gardner max. 2 |
Gardner max. 1 |
Viscosity at 25 °C |
50-80 cps |
250-450 cps |
5000-12000 cps |
Mixing basis |
AEW 168.19 g/eq |
AHEW 92 g/eq |
AHEW 182 g/eq |
phr on YLCE-2021 |
110 at k = 0.85 |
70.8 |
140.0 |
Mix viscosity, calculated |
123 mPa·s |
287 mPa·s |
1956 mPa·s |
Gel at 25 °C |
Not practical |
Workable |
Workable |
Cure heat required |
Staged oven cycle |
Ambient possible |
Ambient possible |
The mass penalty is real: 110 kg of MHHPA per 100 kg of YLCE-2021 against 70.8 kg of YLH-9101 amine hardener. The viscosity gain is larger: a 123 mPa·s mix fills a winding that a 287 mPa·s mix only wets slowly.
YLH-3002 shows the other end: 182 g/eq, 140 kg per 100 kg of the same resin, and a mix near 1956 mPa·s. That is a casting paste, not an impregnation varnish.
Colour cannot be read across columns. Pt-Co and Gardner are different scales, and a Gardner 1 is not a Pt-Co 1. If a sheet mixes them, check which scale the limit belongs to.
One equation sets the dose, and the only judgement inside it is the 0.85 factor that most casting shops apply to an anhydride-epoxy pair.
phr = 100 × AEW ÷ EEW × k, where AEW is the anhydride equivalent weight, EEW the epoxy equivalent weight of the resin, and k the stoichiometric factor.
At k = 1.00 the groups balance. At k = 0.85 the mix runs slightly epoxy-rich, which offsets etherification at high temperature and anhydride lost to hydrolysis in an open bath.
Table 3. MHHPA requirement for four Yolatech epoxy grades, at full stoichiometry and at the 0.85 working factor.
Epoxy grade |
EEW used |
Stoichiometric phr |
phr at k = 0.85 |
Mix viscosity, calculated |
YLCE-2021 |
130 g/eq |
129.4 |
110.0 |
123 mPa·s |
YLSE-0600 |
105 g/eq |
160.2 |
136.2 |
695 mPa·s |
170 g/eq |
98.9 |
84.1 |
567 mPa·s |
|
YLE-128 |
187 g/eq |
89.9 |
76.4 |
1309 mPa·s |
Worked example: 100 kg of YLCE-2021 at 130 g/eq carries 769.2 epoxy equivalents, and 110 kg of MHHPA at 168.19 g/eq carries 654.0 anhydride equivalents. The ratio is 0.850; the batch is 210 kg at 52.4% hardener.
Mix viscosity comes from a log-mixing rule, log η = Σ w log η, with 65 cps for MHHPA and the midpoint of each resin window. It predicts rather than measures, so confirm on a viscometer at 25 °C.
The rule explains the YLE-128 bisphenol A resin row. At 13000 cps it stays near 1309 mPa·s even at 76.4 phr, so that pair belongs in casting, not impregnation.
Accelerator goes in last and shifts gel time more than the MHHPA dose does; check with the supplier before fixing a level.
Four conditions decide whether a casting comes out clear: moisture, mix temperature, degassing and the oven ramp.
• Keep the drum closed between withdrawals; an anhydride takes up water, turns into the diacid and hazes.
• Warm resin and hardener to 50-60 °C before mixing, so the blend degasses.
• Add MHHPA first, stir without air entrapment, then accelerator.
• Degas under vacuum at mix temperature; low viscosity releases air fast and lets fillers settle fast.
• Impregnate at 60-80 °C until bubbling stops. Cold varnish on a cold coil is the usual cause of voids.
• Gel at 100-120 °C, post-cure at 140-160 °C, and ramp slowly above 20 mm.
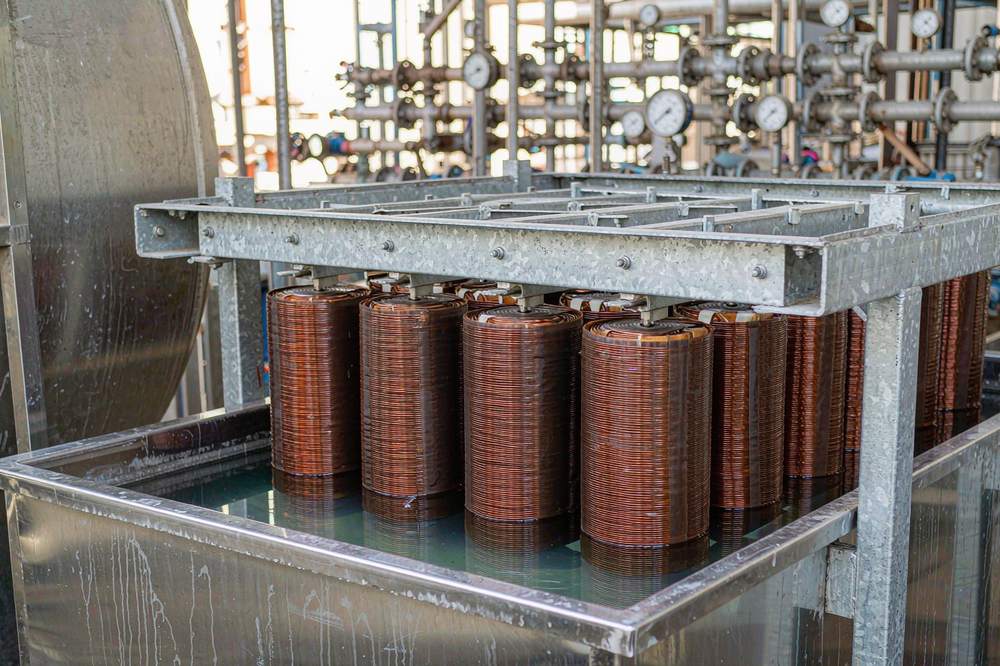
Figure 2. Coil impregnation is where the 50-80 cps band matters most, because the varnish has to displace air from the winding before gel.
The published application list is narrow and electrical: coil impregnation, component casting, and sealing of semiconductors such as insulators, capacitors, LED and digital tubes.
Table 4. Published application routes for MHHPA and the line check that matters for each.
Process route |
Published fit |
Line check |
Coil impregnation |
Thin varnish wets fine wire |
Bath viscosity and water |
Insulator casting |
Fills thin walls before gel |
Mould temperature spread |
Capacitor and LED potting |
Clear, colour-stable casting |
Pt-Co of each incoming lot |
Semiconductor sealing |
No amine residue to blush |
Cure completeness by DSC |
Coating resin intermediate |
Anhydride for polyester routes |
Acid value and water |
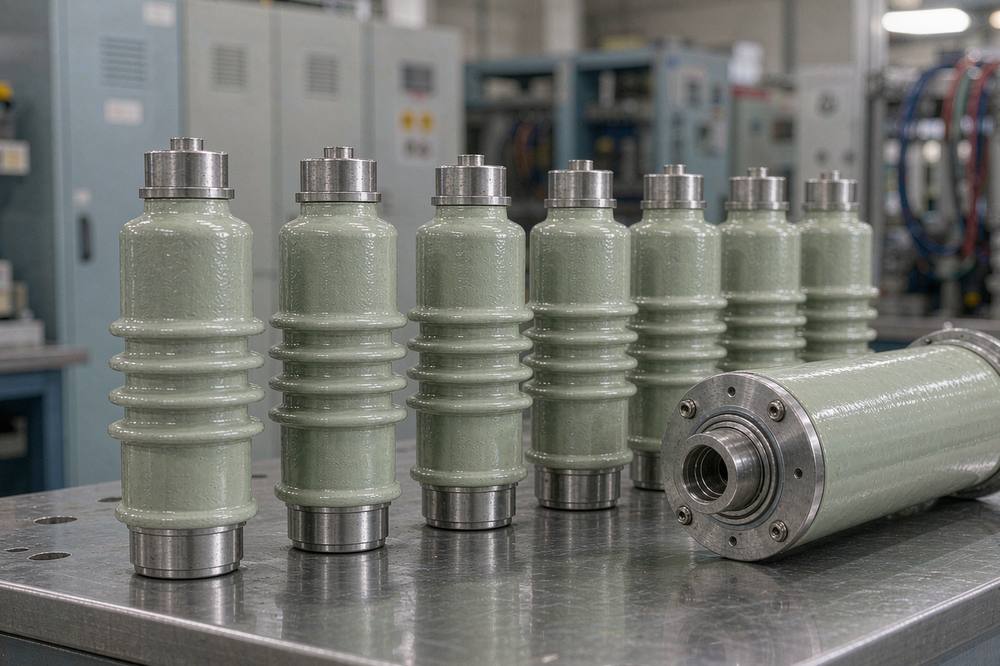
Figure 3. Cast insulators and potted components are the visible end use; the Pt-Co limit on the hardener keeps the cast body water-clear.
MHHPA is the wrong hardener for anything that must cure below 100 °C, and its storage window is narrower than the resin it cures.
Ambient-cure flooring, hand lay-up and field repair are out. The chemistry needs an oven, and no accelerator turns it into a 25 °C system with usable pot life.
Cold storage is the second trap. Below -15 °C the liquid freezes; remelt at 60 °C or lower with the lid on, because an open drum pulls in water faster than the crystals melt.
Low viscosity cuts both ways. Fillers settle overnight, and thin varnish finds every gap in a worn mould.
Shelf life is 12 months against 24 for YLCE-2021, so rotate stock; if a drum sat a year, verify water first.
Each lot should be checked against the COA on four lines: content at 98% minimum, Pt-Co at 50 maximum, viscosity at 50-80 cps at 25 °C, and iodine value at 1.0 maximum.
Water has no published limit. Set one from the first COA and run viscosity in duplicate at 25 °C; a single reading on a cold sample misleads.
Anhydrides are skin and respiratory sensitisers. Gloves, goggles and ventilation are the minimum, the SDS governs, and spills go to absorbent rather than to a drain.
Full stoichiometry gives 129.4 phr; the 0.85 factor gives 110 phr, or 110 kg per 100 kg of YLCE-2021. Recalculate for other resins with phr = 100 × 168.19 ÷ EEW × 0.85.
Because the ring-opening cure is slow at room temperature. A liquid hardener solves metering only; the hydroxyl attack that starts the chain needs heat.
No. The dose moves from 70.8 to 110 phr on the same resin, the cure needs heat, and pot life stretches from hours to days. Reformulate the accelerator and the schedule.
It measures residual unsaturation in the ring. A low value means the 3,4-methyl hexahydrophthalic anhydride is fully hydrogenated, so no aromatic chromophore is left to yellow the casting.
Drums and IBC tanks at 5-30 °C, dry and sealed, for 12 months. If it freezes, remelt at 60 °C or below with the lid on and mix before use; water pickup during remelt is the real risk.
No. Those processes need an ambient-cure amine. MHHPA belongs in heated impregnation, casting and potting lines.
MHHPA is a colorless liquid anhydride with 50-80 cps at 25 °C, 98% minimum assay, a freezing point at or below -15 °C and an iodine value capped at 1.0.
Its 168.19 g/eq sets 110 phr on a 130 g/eq alicyclic epoxy at the 0.85 factor, and the mix lands near 123 mPa·s.
That suits heated impregnation, insulator casting and potting. It does not suit room-temperature cure, and it does not rescue a 13000 cps bisphenol A resin.
1. Yolatech product page: https://www.yolatech.com/34-methyl-hexahydrophthalic-anhydride-cas-no-25550-51-0-mhhpa (accessed 2026-10-19).
2. Yolatech product page for YLCE-2021 alicyclic epoxy: https://www.yolatech.com/34-epoxycyclohexylmethyl-ylce-2021-cas-2386-87-0 (accessed 2026-10-19).
3. Yolatech product page for YLH-9101: https://www.yolatech.com/curing-agnet-ylh-9101 (accessed 2026-10-19).
4. Yolatech product page for YLH-3002: https://www.yolatech.com/curing-agnet-ylh-3002 (accessed 2026-10-19).
5. Yolatech Technical Data Sheet, Material Safety Data Sheet and Certificate of Analysis for MHHPA 25550-51-0 (available on request).
6. ASTM D1652, epoxy content of epoxy resins.
7. ISO 3001, determination of epoxy equivalent.
8. ASTM E203, water content by Karl Fischer titration.
9. ISO 3679, flash point, rapid equilibrium closed cup.
 IPv6-Netzwerk unterstützt